A Dust Hazard Analysis (DHA) should help a facility understand where combustible dust can cause a fire, flash fire, or explosion, determine whether existing safeguards are adequate, and identify the actions needed to reduce risk. Its value depends on how well the analysis reflects the materials, equipment, and work practices at the site.
Common DHA mistakes include relying on unsuitable test data, overlooking hidden dust deposits, assuming installed protection is adequate, and leaving recommendations unresolved. These gaps can affect both safety decisions and capital spending. A facility may invest in a new dust collector while leaving a connected process or an ignition source insufficiently evaluated.
For EHS managers, plant managers, and engineers preparing a new DHA or reviewing an existing one, the following ten mistakes provide a practical starting point.
1. Accepting an SDS as proof that a dust is safe
A Safety Data Sheet (SDS) is an important input, but silence about dust explosion hazards does not establish that a material is safe. In its 2006 combustible dust study, the U.S. Chemical Safety Board identified substantial gaps in the hazard information provided by the data sheets it examined.
How to avoid it: Review the material as it is actually processed. Ask whether cutting, grinding, drying, or collection produces a different form from the supplied product. Use applicable existing evidence or appropriate testing to establish the hazard basis, and document what remains uncertain. A generic statement such as “not regulated for transportation” does not answer the process dust hazard question.
2. Testing a sample that does not represent the process
The incoming product may differ from fines collected downstream. ASTM E1226 explains that measured explosibility values depend on the sample and test method; they are not universal constants for a material name.
How to avoid it: Define where each sample comes from and which operating condition it represents. Review particle size, moisture, formulation, contamination, recycled material, and foreseeable variation. Explain any drying, sieving, or milling performed before testing. The aim is a defensible representation of the hazard, including reasonably foreseeable adverse conditions. Artificially changing the sample without explaining its relevance can also produce misleading design inputs.
3. Using Kst as the only measure of risk
Kst and Pmax describe aspects of dust explosion severity under test conditions. They do not establish how easily a dust will ignite. Minimum Ignition Energy (MIE) testing addresses sensitivity to spark ignition, which is a different question.
A low Kst does not, by itself, justify a low overall risk rating. Likewise, a negative dust-cloud explosibility result does not resolve layer ignition or bulk self-heating hazards. ASTM E1226 expressly limits what can be inferred about these other combustion behaviors.
How to avoid it: Select tests to support the decisions in the DHA. Avoid treating every available test as automatically necessary for every sample. The relevant questions may include the following.
| Engineering question | Information to consider |
| Could a spark ignite the dust cloud? | MIE and the credible discharge mechanisms. |
| Could hot equipment ignite a dust cloud or deposit? | Dust layer and cloud ignition temperatures, as applicable. |
| Could stored powder heat itself to ignition? | Self-heating behavior under relevant storage conditions. |
| Can an inerting strategy provide protection? | Limiting Oxygen Concentration and a suitable control-system design basis. |
HazBasis can help scope combustible dust testing and self-heating and thermal instability testing around the questions your process needs to answer.
4. Reviewing only the dust collector and normal operation
A collector-focused review can leave gaps at bag dumps, mills, mixers, dryers, conveyors, silos, packaging stations, and waste handling areas. Normal production is only one operating condition. Startup, shutdown, filter replacement, equipment cleaning, maintenance, blockages, and loss of extraction can change the hazard scenario.
How to avoid it: Define the equipment and building areas within the DHA scope, then trace material movement and the connections between them. For each operation, ask where dust can be released, dispersed, accumulated, or ignited. Include operator exposure during open handling: an unconfined dust cloud can cause a flash fire even where pressure-producing confinement is absent.
5. Overlooking hidden dust and secondary explosions
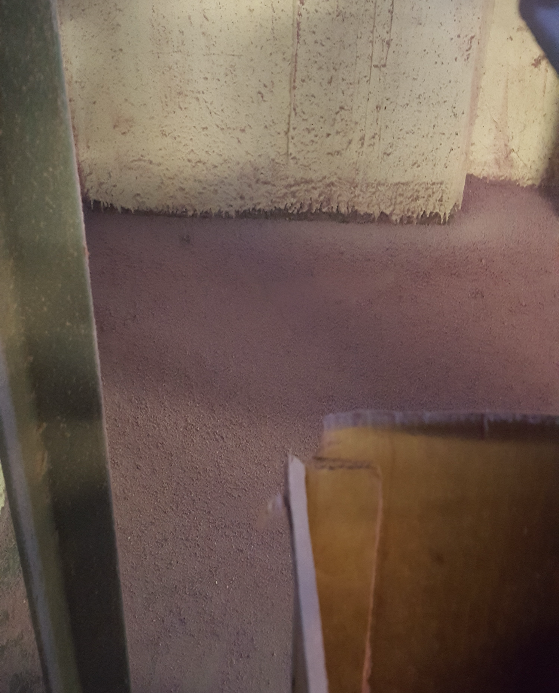
A clean floor does not establish that the building is free from hazardous dust accumulations. Beams, cable trays, ledges, equipment tops, and concealed spaces can hold dust that becomes airborne during an initial event. The CSB recommendations following the Imperial Sugar explosion specifically addressed overhead surfaces as well as equipment and floors.
How to avoid it: Document accumulation locations, release sources, inspection access, cleaning responsibilities, and suitable removal methods. Set housekeeping criteria using the material properties, affected area, and applicable requirements. Do not use a single visual thickness rule as a universal safe limit. Cleaning practices also need review because dispersing deposits can create an ignitable cloud.
6. Limiting ignition source analysis to electrical equipment
An electrical area classification drawing does not answer every ignition question. The DHA also needs to consider friction, overheated bearings, mechanical impact, hot work, hot surfaces, smoldering material, self-heating, and electrostatic discharges. Which sources are credible depends on the operation and the material.
How to avoid it: Evaluate how ignition could occur during each operating mode. Check bonding and grounding where relevant, but also assess insulating hoses, liners, containers, and flexible packaging. A grounding connection alone does not demonstrate that electrostatic hazards have been controlled. Relate material ignition sensitivity to the actual discharge mechanism and safeguards.
Coordinate hazardous area classification with an electrostatic hazard analysis where those reviews are needed. Their findings should feed into the DHA.
7. Assuming a vented collector protects the whole system
The presence of an explosion vent is only part of a protection assessment. A DHA should examine the collector, connecting ducts, upstream and downstream equipment, return-air paths, and the people or structures exposed to a discharge. HazBasis includes these interfaces in its dust collector and explosion protection review.
How to avoid it: Verify the protection design against the material data, equipment configuration, pressure capability, operating conditions, and manufacturer limitations. Evaluate explosion isolation where required, the location of vent discharge, and the suitability of any suppression or flameless venting system. Confirm inspection, testing, and maintenance responsibilities.
A useful review question is: What evidence shows that each safeguard will perform its intended function in this specific scenario? A purchase order, equipment label, or photograph alone may not answer it. Detailed protection design should be completed by personnel competent in the applicable design methods.
8. Using a generic checklist without process knowledge
Checklists can improve consistency, but a completed checklist can still miss why a hazard exists. For example, “dust extraction provided” does not establish whether extraction remains effective when two lines operate together or whether a bypass changes the exposure.
How to avoid it: Use a qualified DHA leader and involve people who understand operations, maintenance, engineering, and EHS at the facility. Ask operators about recurring jams, temporary fixes, unusual odors, smoldering events, and conditions on less frequently observed shifts. Record the technical reasoning behind conclusions, including assumptions and unresolved information needs.
Recommendations should follow identifiable scenarios. “Improve dust control” is difficult to implement; identifying the release point, affected operation, required evaluation, and acceptance criteria gives the facility a task it can manage.
9. Leaving recommendations without owners or closure evidence
A DHA report cannot reduce risk unless the facility acts on its findings. Recommendations often lose momentum when nobody owns them, engineering questions remain unresolved, or completed purchases are treated as proof that the hazard has been addressed.
How to avoid it: Maintain an action register that records the finding, responsible person, priority and rationale, target date, interim measures where needed, and closure evidence. Distinguish a recommended safeguard from one already installed and verified. Proposed equipment should not be credited as an existing safeguard.
For example, closing an extraction improvement may require installation records and evidence that the system performs adequately under the relevant operating conditions. Review overdue actions with management, and document the technical basis for any alternative solution.
10. Treating the DHA as a one time report
A DHA can become outdated when a facility changes its raw materials, throughput, equipment, ductwork, filters, storage arrangements, or work practices. Incident and near-miss findings can also reveal that an earlier assumption was incomplete.
How to avoid it: Connect the DHA to management of change and assess relevant changes before implementation. Maintain a documented schedule for periodic review and revalidation that follows the applicable standard and facility requirements. A scheduled review date should not delay the assessment of a material change.
Define the standards basis explicitly, including the edition of NFPA 660 used, relevant industry provisions, and adopted code requirements. Older reports may reference NFPA 652 or NFPA 654; updating a title page does not demonstrate that their technical conclusions remain valid. Review the governing requirements with the appropriate authority and project stakeholders.
Questions to ask before accepting a DHA
Before issuing or accepting the report, ask whether it gives your team clear answers to these questions:
- Does the material evidence represent the dust and conditions actually evaluated?
- Are the process boundaries, operating modes, and important assumptions documented?
- Are credible fire, flash fire, and explosion scenarios connected to specific safeguards?
- Is there evidence that credited safeguards are suitable and maintained?
- Can each recommendation be assigned, implemented, and verified?
- Are future changes and periodic revalidation addressed?
Frequently asked questions about DHA mistakes
Is combustible dust testing the same as a DHA
No. Testing characterizes selected material properties. A DHA combines the relevant evidence with process conditions, equipment, operating practices, and safeguard information to evaluate hazards at the facility. A laboratory report is an input to that analysis.
Does a low Kst mean explosion protection is unnecessary
No. Protection decisions also depend on the process scenario, equipment strength, confinement, ignition potential, and applicable requirements. Kst should be interpreted within the complete engineering assessment.
Do all materials need the same dust testing package
No. The testing scope depends on the available evidence and decisions the DHA must support. Existing data may be useful when its applicability is justified. Missing information should be identified and resolved before relying on conclusions that depend on it.
Can an existing DHA be updated
Yes. Review the existing report against current materials, equipment, operating conditions, standards basis, and action status. The extent of revision depends on the changes and the quality of the original analysis. Some gaps may require additional site review, testing, or engineering work.
Get practical support for your Dust Hazard Analysis
HazBasis Process Safety supports Dust Hazard Analysis, combustible dust testing, ignition source evaluation, and related process safety reviews. We help facilities connect material data with process conditions and identify practical actions for managing combustible dust hazards.
If you are planning a new DHA, reviewing an older report, or deciding which dust tests are needed, send us your process description, equipment list, available SDSs, and existing test reports. We can help define the appropriate scope.